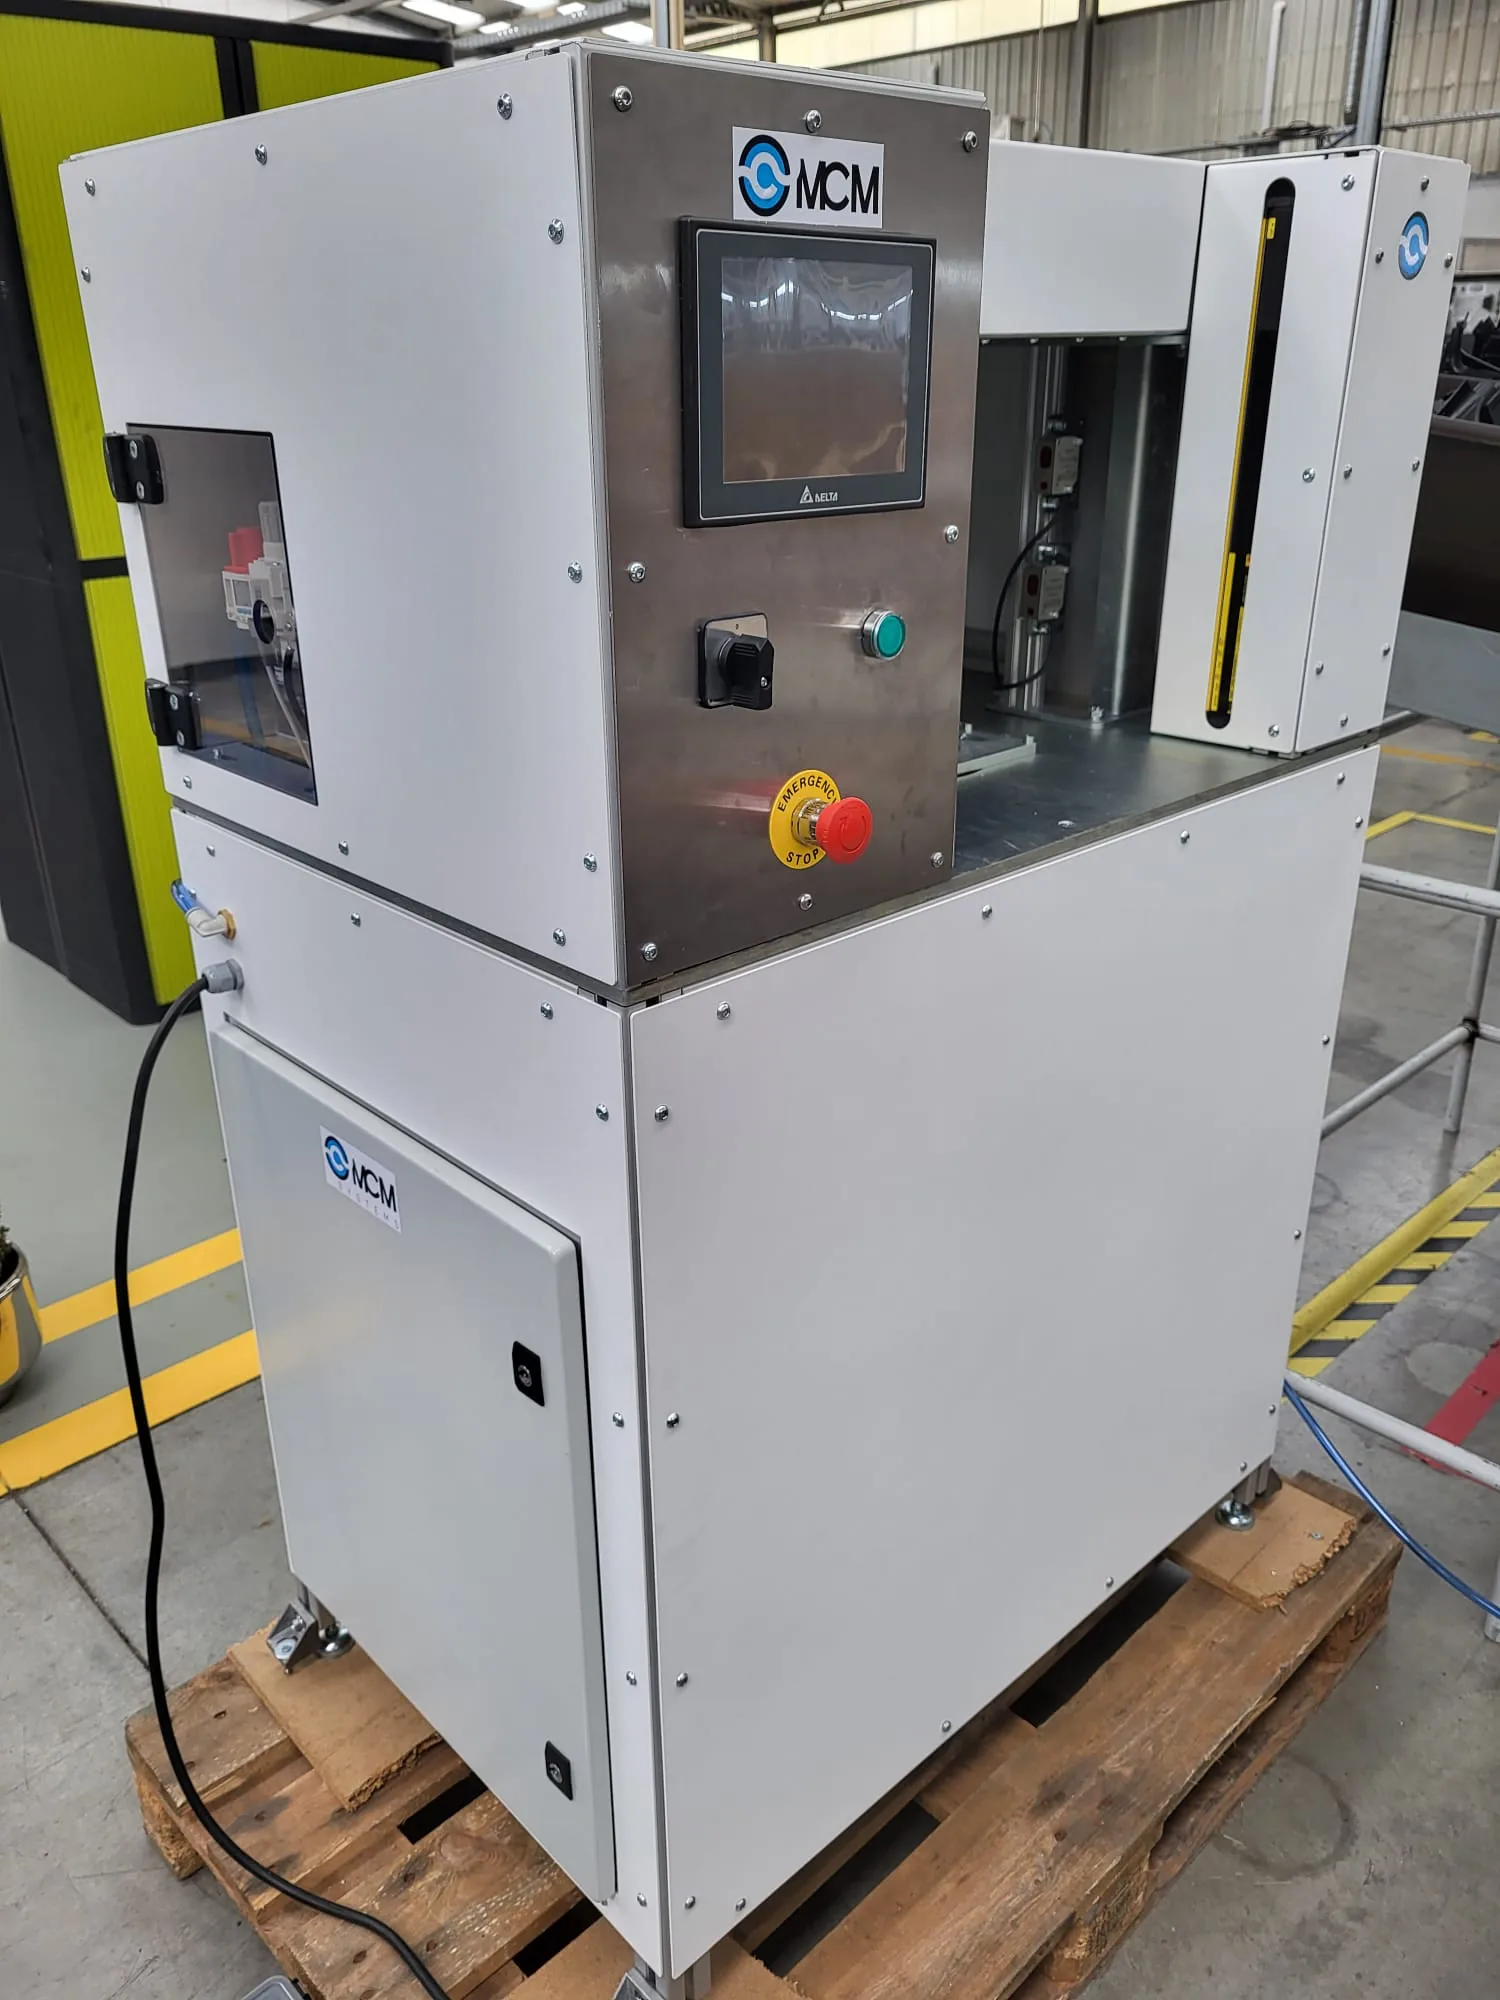
What is a functional test system?
A functional test system checks whether a product performs as intended rather than only checking how it looks. Depending on the application, the station can stimulate inputs, measure outputs, verify communication, test pressure or leaks, check light behaviour and confirm that required components respond correctly.
Why production testing is different from laboratory testing
A production station must repeat the same sequence within the available cycle time while remaining safe and straightforward for operators. Product positioning, connectors, pneumatic movements, sensors, test equipment, software and HMI all need to work as one system.
Typical elements of a custom test station
- Dedicated mechanical fixture and product positioning
- Electrical and pneumatic control
- Measurement instruments and sensors
- Automated test sequence and pass/fail limits
- Operator HMI and diagnostic information
- Result storage and traceability
Traceability turns a test into production data
When each result is associated with a product, batch or serial number, the station can provide useful evidence for quality teams and process improvement. Stored measurements also make it easier to investigate recurring failures instead of relying only on a final pass/fail count.
Custom engineering around the product
MCM develops functional test systems around the required validations and production constraints. Previous applications include electrical characteristics, leak tests, light-quality checks, communication tests and component detection, combined with dedicated jigs, safety and traceability.
Explore Functional Test Systems or discuss a custom test requirement with MCM.
 English
 Portuguese
 French
 Spanish