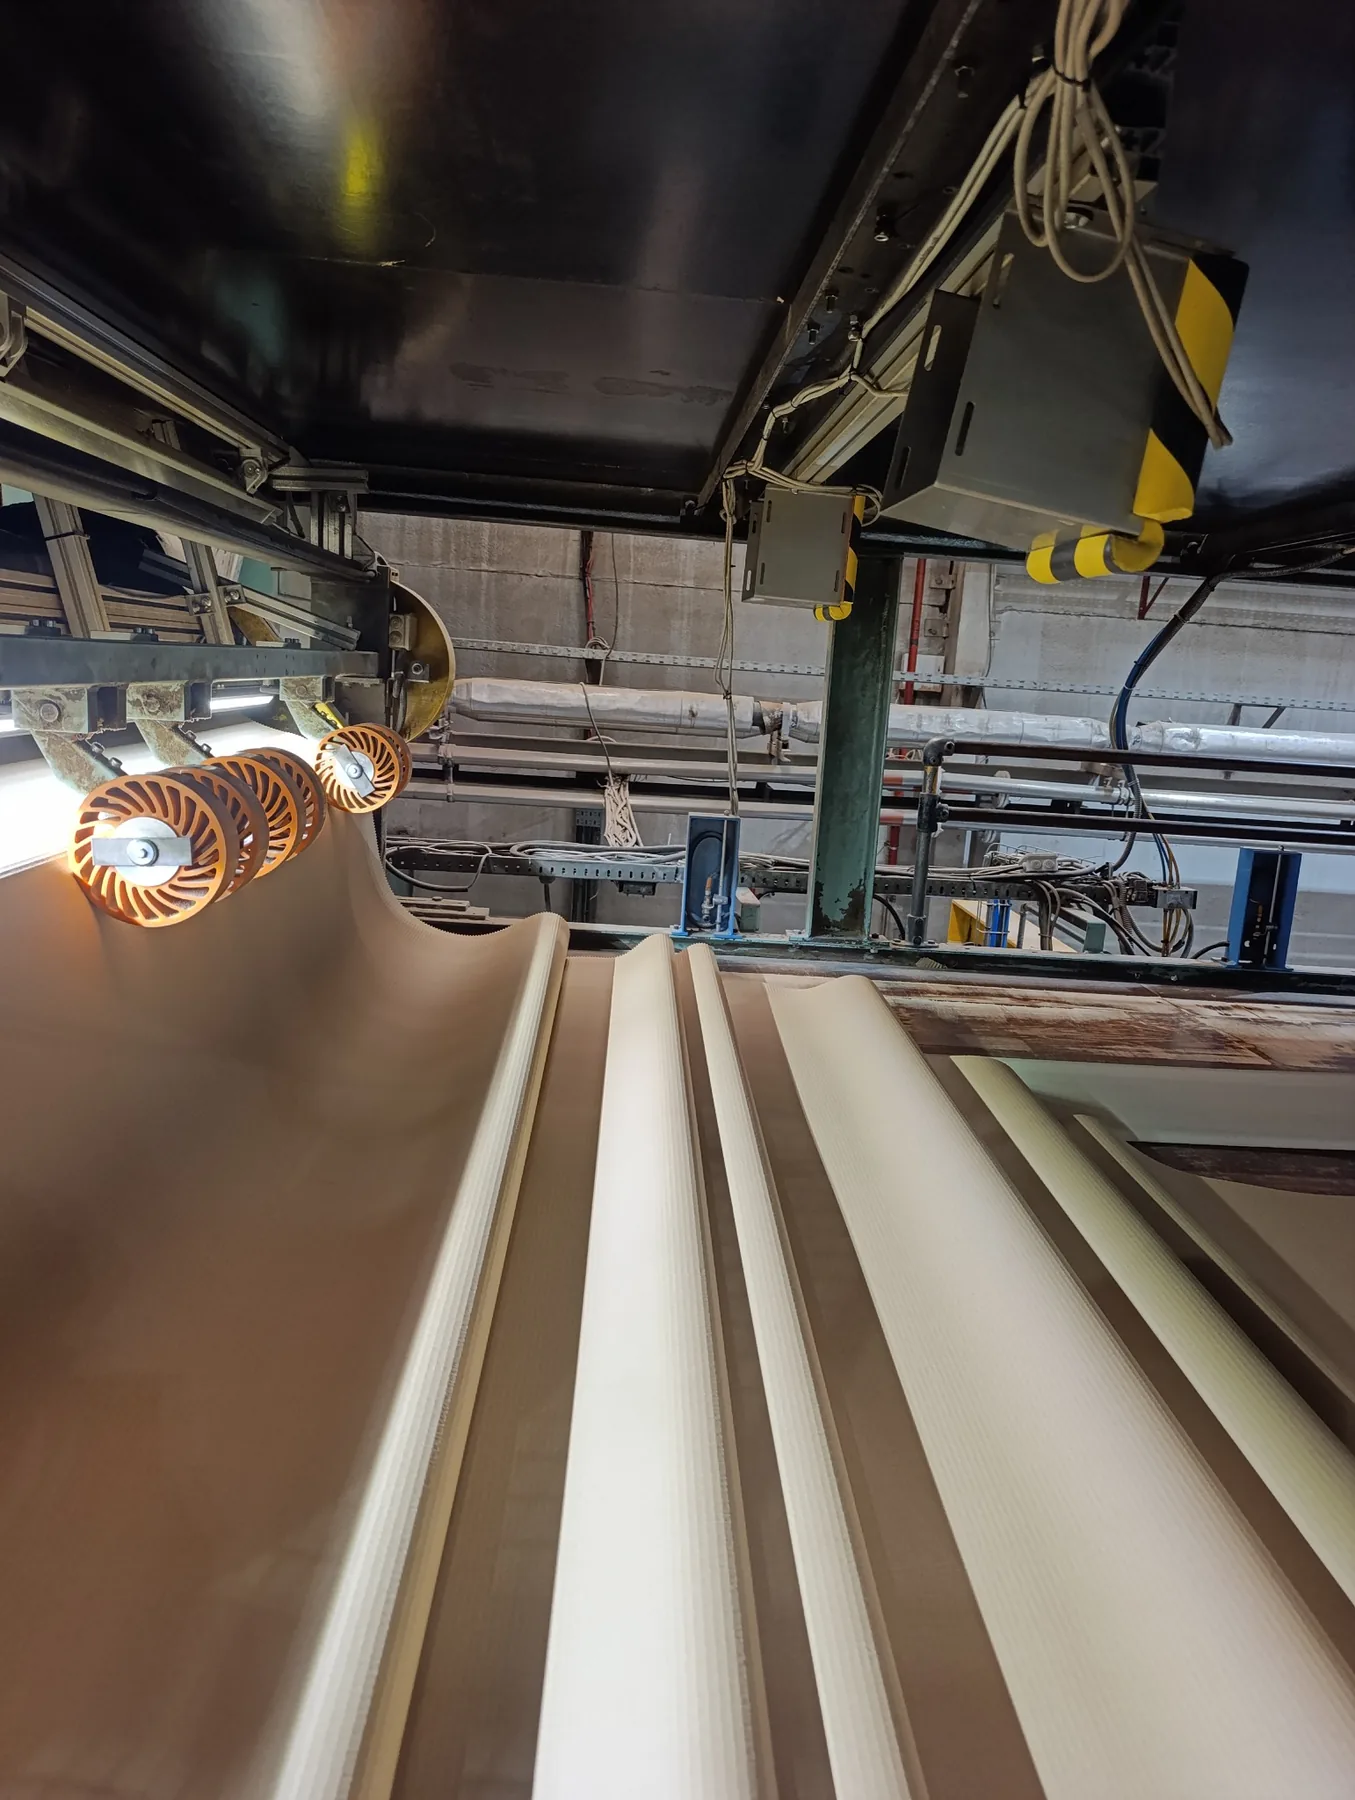
What is machine vision?
Machine vision is the use of cameras, controlled lighting, optics and image-processing software to inspect products or guide decisions in an industrial process. Unlike a manual visual check, a properly engineered system can apply the same inspection criteria repeatedly and connect the result directly to the production line.
The objective is not simply to take a good image. The objective is to make a reliable production decision: pass the product, reject it, alert an operator, stop a process or record a result for traceability.
How an industrial vision system works
A typical project starts with the product and the defect. Engineers define what must be visible, how much variation is acceptable, the available inspection time and what should happen after the decision. Lighting and optics are selected to make the relevant feature stable before software evaluates the image.
- Camera: acquires the image at the required resolution and speed.
- Lighting: creates repeatable contrast and reduces unwanted variation.
- Optics: defines field of view, working distance and image detail.
- Software: measures, classifies or detects the required feature.
- Automation: communicates the result to PLC, reject mechanism, HMI or traceability system.
Where machine vision is used
Common applications include presence and position checks, assembly verification, print and colour control, dimensional inspection, surface inspection and product orientation. In packaging, electronics and automotive production, several checks can be combined in one station.
Rule-based vision or deep learning?
Rule-based tools are effective when the feature can be described consistently with geometry, contrast, colour or measurement limits. Deep learning can help when acceptable and defective appearances vary in ways that are difficult to describe with fixed rules. The right approach depends on real samples, process variation and the cost of false decisions.
Why integration matters
A vision algorithm is only one part of a production system. Mechanical stability, electrical design, operator workflow, line communication and traceability determine whether the inspection remains useful after commissioning. MCM designs these elements around the application so that the inspection works as part of the production process.
Explore MCM machine vision and quality-control solutions or send us your application for a feasibility review.
 English
 Portuguese
 French
 Spanish